Evolve Medical
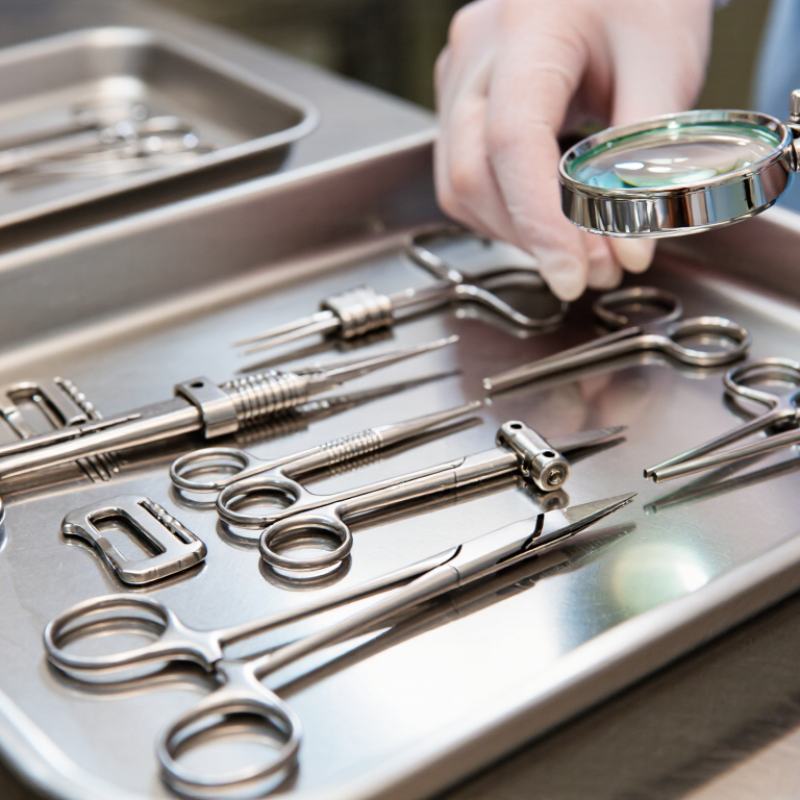
How to identify high-quality stainless steel surgical tools begins with more than a bright, mirror-like finish. A polished surface can hide weak joints, poor machining, or unsuitable steel. Experienced technicians inspect each instrument under strong, even light. They check the working edges, box locks, serrations, and handles. The surfaces should appear smooth, consistent, and free from pits, stains, sharp burrs, or uneven grinding. Hinged tools should open and close without grinding. They should not feel loose or unusually stiff. Small details matter.
Material verification provides stronger evidence. Reputable manufacturers should identify the stainless steel grade and provide traceable quality documentation. Common medical grades may include 316L, but the correct choice depends on the instrument’s function and sterilization conditions. Magnetic behavior alone cannot confirm a steel grade. It is only a limited screening clue. Weight, balance, and handle comfort also reveal manufacturing quality during repeated handling. A reliable tool should maintain its alignment after cleaning and sterilization. Its markings should remain readable, not fade after several cycles. I would not accept a certificate without checking whether it matches the actual batch. That step is sometimes overlooked. It should not be.
Quality assessment should combine visual inspection, functional testing, material records, and supplier history. Independent testing may be appropriate when documentation is incomplete or performance seems inconsistent. No single feature proves that an instrument is safe or durable. Careful evaluation reduces avoidable failures, protects clinical workflow, and supports informed purchasing decisions.
Material composition is the first serious test of a surgical tool. “Stainless steel” is not one material. During supplier audits, I check the mill certificate, heat number, and surface condition before judging appearance. ASTM F899 identifies accepted stainless steel families for surgical instruments, while ISO 7153-1 provides material guidance for surgical applications.
Austenitic 316L contains roughly 16–18% chromium, 10–14% nickel, and 2–3% molybdenum. Its low carbon content, normally below 0.03%, supports corrosion resistance after welding. It suits some handles and components, but softness can limit cutting performance. Martensitic grades, such as 420, typically contain about 12–14% chromium and gain hardness through heat treatment. Grade 440A contains approximately 16–18% chromium and higher carbon, supporting sharper edges but requiring careful corrosion control.
Hardness is only part of the evidence. A 2023 World Stainless statistical release reported global stainless crude steel production at about 58.4 million tonnes. High output does not guarantee medical-grade consistency. Batch control still matters. Ask for chemical analysis, hardness results, and sterilization testing. Portable XRF can verify chromium and nickel, but it cannot reliably measure carbon. That weakness is easy to overlook. A polished surface may hide poor heat treatment or chromium depletion. In practice, I would combine laboratory verification with repeated cleaning, autoclave exposure, and microscopic inspection. Some purchasing checklists remain too simple. Grade names alone are not enough.
How to Identify High Quality Stainless Steel Surgical Tools
Precision, Design, and Manufacturing Quality
A reliable surgical tool begins with controlled geometry. During hands-on inspection, I check whether jaws meet evenly and move without lateral play. Smooth action matters. Handles should feel balanced, not merely polished. Fine serrations must be consistent, with no flattened teeth or sharp burrs. Small defects can affect control during delicate procedures.
Material selection also deserves close attention. High quality stainless steel should have documented composition, corrosion resistance, and appropriate hardness. A bright surface does not prove quality. Poor finishing can hide weak edges or contamination. Look for uniform passivation, clean joints, and surfaces that tolerate repeated professional processing. Technical documents should identify inspection methods, material records, and relevant quality requirements.
Manufacturing discipline separates acceptable tools from dependable ones. I examine welds, hinges, locking systems, and laser markings under strong light. Traceability is valuable when a tool requires review or replacement. Dimensional checks should follow defined tolerances, not personal judgment alone. Functional testing should include repeated opening, closing, and locking cycles. One imperfect detail deserves attention. A loose hinge today may become a serious handling problem later.
Even experienced inspectors can overvalue appearance. I once noticed that a flawless finish made a poorly aligned tip seem acceptable. That mistake changed my inspection habits. I now compare tools against calibrated gauges, documented specifications, and practical handling requirements. Reliable quality is visible in design, measurable in manufacturing, and confirmed through consistent inspection records.
Precision, design, and manufacturing quality begin with selecting the right stainless steel grade. This chart compares representative nominal alloy compositions commonly associated with surgical instruments.
Chromium supports corrosion resistance, nickel improves toughness and formability, and molybdenum enhances resistance to localized corrosion. Austenitic 316L is valued for corrosion resistance, while martensitic 420 and 440A are commonly selected when edge retention and hardness are more important. Actual compositions vary by applicable material specification and heat treatment.
When evaluating stainless steel surgical tools, I start with the surface, not the packaging. Under bright, angled light, a good finish looks even and feels smooth against a gloved fingertip. There should be no pits, drag marks, sharp edges, or cloudy patches around joints. Tiny scratches can trap soil and moisture. That matters during cleaning. A mirror finish is not automatically better. Some working surfaces need controlled texture for grip. I have seen attractive tools fail because their hinges were rough inside. Inspect the overlooked areas.
Sterilization performance depends on the steel, design, and cleaning process together. Instruments should open fully before washing, allowing water and sterilant to reach the hinge. Follow the validated cycle specified by the facility and instrument maker. Repeated steam exposure can reveal weak passivation or trapped residues. After a cycle, inspect for discoloration, residue, and changes in movement. Dry instruments promptly. Moisture left in a box is a quiet problem. One practical check is examining joints after several cycles, not only after delivery. A tool may look perfect on day one.
Corrosion resistance is more than a label saying “stainless.” Chromium content, alloy quality, surface passivation, and chloride exposure all influence performance. Rust-colored spots near joints deserve investigation, even when they appear small. Do not polish them away blindly. Cleaning chemicals, saline residue, and dissimilar metals can create corrosion sites. Keep inspection records with cycle history and recurring defects. My own judgment is not infallible; lighting can hide early damage. When uncertainty remains, consult a qualified materials or sterile-processing professional and request documented test data.
| Evaluation Dimension | What High Quality Looks Like | Practical Benchmark or Requirement | How to Verify | Warning Signs |
|---|---|---|---|---|
| Material Identification | The instrument is manufactured from a documented surgical-grade stainless steel selected for its intended use, such as martensitic steel for cutting edges or austenitic steel for corrosion-sensitive components. | Material grade, heat treatment, and lot traceability should be documented. Common surgical stainless steels include grades within the 400 and 300 series, but the appropriate grade depends on the instrument design. | Review the material certificate, heat-treatment records, and lot number. Where necessary, confirm composition using portable X-ray fluorescence or laboratory analysis. | Unspecified “medical steel,” missing material certificates, inconsistent hardness, or unexplained changes in color or magnetic response. |
| Surface Finish | Surfaces are smooth, uniform, free from pits, folds, burrs, deep scratches, grinding marks, embedded particles, and visible manufacturing residue. | A polished working surface commonly targets a low roughness value, often around Ra ≤ 0.8 µm for critical contact areas. There is no single universal Ra limit for every surgical instrument; the specification should match the design and applicable standard. | Inspect under bright, diffuse lighting and magnification. Measure surface roughness with a calibrated profilometer at representative locations. | Visible pits, orange discoloration, rough transitions, sharp burrs, polishing compound, or scratches that can retain soil and moisture. |
| Passivation | The stainless steel surface has a stable chromium-rich passive layer that reduces the risk of iron contamination and corrosion. | Passivation should be validated using an appropriate procedure, such as ASTM A967 where applicable, with acceptance criteria defined for the instrument and material. | Review the passivation process specification and batch records. Use recognized tests such as water immersion, high-humidity, copper sulfate, or electrochemical testing when appropriate. | Free iron, rust staining after cleaning, unexplained heat tint, or a passivation claim without process controls or test evidence. |
| Dimensional Accuracy | Matched components align correctly, cutting edges meet evenly, jaws close symmetrically, and locking mechanisms operate without excessive play. | Critical dimensions and functional tolerances should be defined on controlled drawings and verified using calibrated gauges or inspection equipment. | Check alignment, jaw contact, tip symmetry, box-lock fit, ratchet engagement, and cutting performance using documented inspection procedures. | Uneven jaw contact, visible gaps, loose joints, binding, excessive force requirements, or inconsistent performance between tools from the same lot. |
| Mechanical Strength | The instrument withstands normal handling, repeated opening and closing, and its intended clinical loads without permanent deformation or cracking. | Mechanical and functional testing should be based on the instrument type, risk assessment, design specification, and applicable national or international standards. | Review design-validation and fatigue-test results. Perform functional cycling and load testing using a documented, reproducible method. | Cracks near joints, distorted tips, premature loss of cutting ability, loose pins, or failure after a small number of operating cycles. |
| Steam Sterilization Compatibility | The instrument tolerates validated steam-sterilization exposure without corrosion, distortion, loss of function, or deterioration of surface finish. | Typical steam cycles may use 121 °C or 132–135 °C, but time, drying, load configuration, and exposure conditions must follow the validated instructions for use. | Confirm validated reprocessing instructions and review testing for repeated cleaning, sterilization, and drying cycles. Inspect instruments after cycling. | Rust after routine sterilization, discoloration caused by heat or residues, seized joints, damaged insulation, or instructions that omit cleaning and drying steps. |
| Cleaning and Soil Removal | The design permits thorough manual or automated cleaning, with accessible joints, smooth transitions, and no unnecessary crevices. | Cleaning instructions should specify disassembly, detergent type, water quality, temperature limits, brushing points, rinsing, lubrication, and drying requirements where applicable. | Review validated cleaning instructions and inspect hinges, serrations, box locks, cannulations, and other soil-retaining areas after simulated use. | Trapped biological material, inaccessible cavities, permanent residue, excessive dependence on manual scrubbing, or unclear detergent compatibility. |
| Corrosion Resistance | The instrument remains free from red rust, pitting, crevice corrosion, and persistent staining during intended use and reprocessing. | Corrosion performance should be verified using a suitable method, such as ASTM F1089 or ISO 13402 where applicable. Results depend on steel grade, finish, cleaning chemistry, water quality, and sterilization conditions. | Review corrosion-test reports and conduct repeated reprocessing trials using representative water, detergents, and sterilization parameters. | Rust spots around joints, pitting on polished areas, corrosion after contact with saline, or failure only explained by improper handling without supporting evidence. |
| Resistance to Cleaning Chemicals | The instrument is compatible with the detergents, enzymatic cleaners, neutralizers, lubricants, and disinfectants specified for its reprocessing route. | Chemical compatibility should be established for the actual concentration, temperature, contact time, and rinse conditions. Chloride-rich or strongly acidic/alkaline residues can increase corrosion risk. | Compare the product instructions with chemical supplier guidance and review compatibility or accelerated-aging test data. | Chloride deposits, etched surfaces, discoloration, cracking, or corrosion associated with unapproved chemicals or inadequate rinsing. |
| Surface Cleanliness | The finished instrument is free from oil, polishing compound, metal debris, adhesive residue, and other contaminants before packaging. | Acceptance limits should be defined by the manufacturer’s validated cleaning process and applicable quality system requirements. | Use visual inspection, white-cloth wipe testing, rinse-water analysis, or validated cleanliness tests appropriate to the instrument. | Oily films, dark residue on wipes, unusual odor, visible particles, or residue emerging during the first cleaning cycle. |
| Packaging and Storage | Packaging protects the finish, cutting edges, tips, and joints from damage, moisture, and contamination during transport and storage. | Packaging should maintain product integrity and provide clear identification, lot traceability, and reprocessing information where applicable. | Inspect packaging seals, protective caps, moisture protection, labeling, and simulated transport results. | Loose instruments rubbing together, damaged tips, wet packaging, missing lot identification, or corrosion visible immediately after opening. |
| Documentation and Quality Control | The supplier maintains controlled specifications, inspection records, risk management, change control, and validated reprocessing instructions. | A quality management system such as ISO 13485 may support consistent production, but certification alone does not prove that a specific instrument has superior finish or corrosion resistance. | Review certificates, inspection plans, nonconformance records, change-control procedures, and validation reports relevant to the instrument. | Generic certificates, unverifiable test reports, no lot traceability, undocumented material substitutions, or unsupported claims such as “rust-proof.” |
How to Identify High Quality Stainless Steel Surgical Tools
Functional Testing and Ergonomic Performance
A high-quality stainless steel surgical tool should feel predictable in the hand. During a hands-on inspection, check the joint, lock, tips, and surface finish. The movement should be smooth, without grinding, sticking, or sudden looseness. Open and close the instrument several times. It should return evenly and maintain alignment.
Test the tool with an appropriate training material, following approved clinical procedures. Scissors should cut cleanly from the hinge to the tip, rather than crushing material. Clamps should close evenly and hold without excessive force. Fine instruments need accurate tip contact under gentle pressure. A bright finish alone proves little. Function matters more.
Ergonomics becomes clear after repeated handling. The finger rings should fit comfortably, even with gloved hands. Handles must provide control without sharp edges or pressure points. A balanced instrument reduces unnecessary wrist movement during detailed work. Check visibility around the working end. Poor balance can cause fatigue. I have learned that a tool may pass a quick test yet feel awkward after several minutes. That weakness deserves documentation, not dismissal. Record the test conditions, observed resistance, alignment, and any change after cleaning or sterilization. A careful review by trained personnel supports safer selection and more consistent performance.
High-quality stainless steel surgical tools begin with credible certification. Look for a documented quality system, such as ISO 13485, and verify its current status. Certification should cover the actual manufacturing site, not only a trading office. Ask for material certificates identifying the steel grade, heat number, and applicable testing. A polished surface is useful evidence, but it proves very little alone.
Traceability must continue from raw steel to finished instrument. Each batch should connect to inspection records, machining details, heat treatment, and final cleaning checks. On the factory floor, I would compare markings, packing labels, and test documents. Small mismatches matter. They may reveal weak document control or simple human error. Either way, the supplier should explain the cause and corrective action clearly.
Supplier reliability appears through repeated behavior. Request production samples, inspection reports, and realistic delivery records. Evaluate how the supplier handles a rejected instrument, a dimensional concern, or a missing certificate. Fast replies are helpful, but complete answers matter more. A reliable partner welcomes audits and shares process limitations honestly. One uncomfortable lesson is that a low price can hide unstable inspection practices. Still, even established suppliers may make mistakes. Review performance regularly, retain batch records, and avoid trusting certificates without checking the physical tools.
It should move smoothly, without grinding, sticking, or sudden looseness. The joint should feel predictable.
Open and close them several times. Test them on approved training material. They should cut cleanly from hinge to tip.
Its jaws should close evenly and hold material without excessive force. Uneven closure needs further review.
Check tip contact under gentle pressure. The tips should align accurately, without visible gaps or harsh pressure.
Finger rings should fit gloved hands comfortably. Handles should avoid sharp edges and pressure points. Balance should limit wrist movement.
No. Appearance alone proves very little. Functional testing, material records, and inspection evidence matter more.
Request a current quality certificate covering the actual manufacturing site. Material documents should identify steel grade, heat number, and testing.
Match instrument markings with packing labels and inspection records. Traceability should cover raw steel, machining, heat treatment, and cleaning.
Request samples, inspection reports, and realistic delivery records. Observe how rejected tools and missing certificates are handled.
Do not trust certificates without checking physical tools. A low price may hide unstable inspections. Established suppliers can also make mistakes.
How to identify high-quality stainless steel surgical tools begins with evaluating their material composition and stainless steel grade. Reliable instruments are made from corrosion-resistant, medical-grade steel with a composition suited to repeated sterilization and demanding clinical use. Their precision, design, and manufacturing quality should be reflected in smooth alignment, accurate joints, consistent dimensions, and carefully controlled workmanship. Well-designed tools should operate smoothly without excessive looseness, sharp edges, or visible manufacturing defects.
Surface finish is also essential: polished, uniform surfaces help resist corrosion, staining, and contamination while supporting effective cleaning and sterilization. Functional testing should confirm that cutting, grasping, clamping, or dissecting tools perform consistently, while ergonomic handles provide comfort, balance, and secure control during extended use. Finally, certification, batch traceability, quality records, and dependable supplier support provide confidence in product consistency and accountability. By reviewing these factors together, purchasers can select surgical tools that offer durability, safety, performance, and long-term value.