 Evolve Medical
High-sensitivity point-of-care lateral flow assays calibrated for tropical climate stability and rapid clinical triage in Western Uganda.
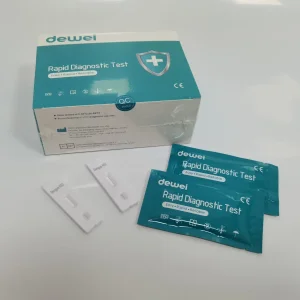
Mbarara City serves as the economic, academic, and clinical epicenter of Western Uganda. Serving a catchment population of over 5 million people across the Ankole sub-region and neighboring districts such as Bushenyi, Ntungamo, and Sheema, Mbarara's healthcare system is anchored by institutions like the Mbarara Regional Referral Hospital (MRRH) and the Mbarara University of Science and Technology (MUST). Consequently, the demand for high-grade, rapid in-vitro diagnostics (IVD) has expanded exponentially.
Healthcare providers, private diagnostic laboratories, NGO clinics, and district health offices in Mbarara face unique logistical and operational environments. The regional climate requires diagnostic lateral flow strips that possess exceptional thermal stability (WHO Zone IVb stability ratings), high resistance to humidity during transport along the Northern Corridor from Mombasa/Entebbe, and long shelf lives (24 months minimum) without requiring continuous active refrigeration.
As a global OEM/ODM manufacturer, Hebei Evolve Medical Technology Co., Ltd. bridges the gap between state-of-the-art diagnostic manufacturing and the localized clinical demands of Mbarara. By delivering standardized, high-sensitivity point-of-care rapid test kits, we support local clinicians in making fast, accurate diagnostic decisions for acute infectious diseases, maternal-child health parameters, and routine screening protocols.
Understanding the microfluidic bio-engineering and reagent formulation behind our diagnostic test strips optimized for tropical distribution.
Our lateral flow test strips utilize monodisperse colloidal gold nanoparticles (40nm diameter) covalently conjugated to monoclonal antibodies against specific targets such as Dengue NS1 protein or Plasmodium falciparum PfHRP-2. This delivers ultra-high optical contrast on nitrocellulose membranes, eliminating ambiguous visual readings even in low-resource clinic settings around Mbarara.
To withstand humidity and thermal shifts in Equatorial Africa, each diagnostic cassette is individually hermetically sealed in composite aluminum foil with high-capacity silica gel desiccants. This ensures zero water vapor transmission rate (WVTR), protecting fragile enzymes and recombinant antigens against hydrolytic degradation during long-term storage.
To reduce cross-reactivity between malaria species (P. falciparum vs. P. vivax) or arboviruses (Dengue vs. Zika/Chikungunya), our proprietary membrane capture zones employ recombinant antigens synthesized in E. coli expression systems. This guarantees diagnostic specificity exceeding 99%, critical for differential diagnosis in Western Uganda clinics.
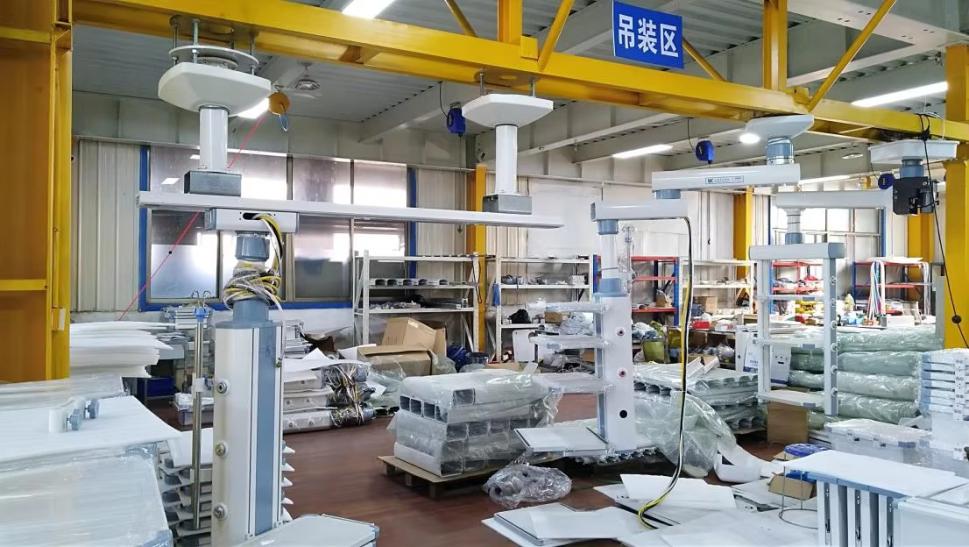
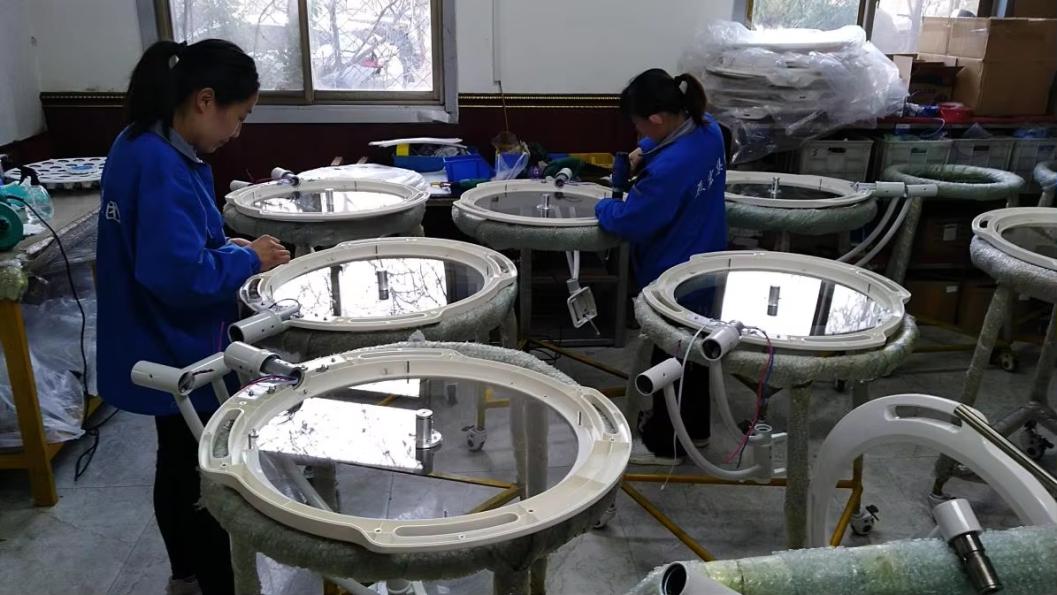
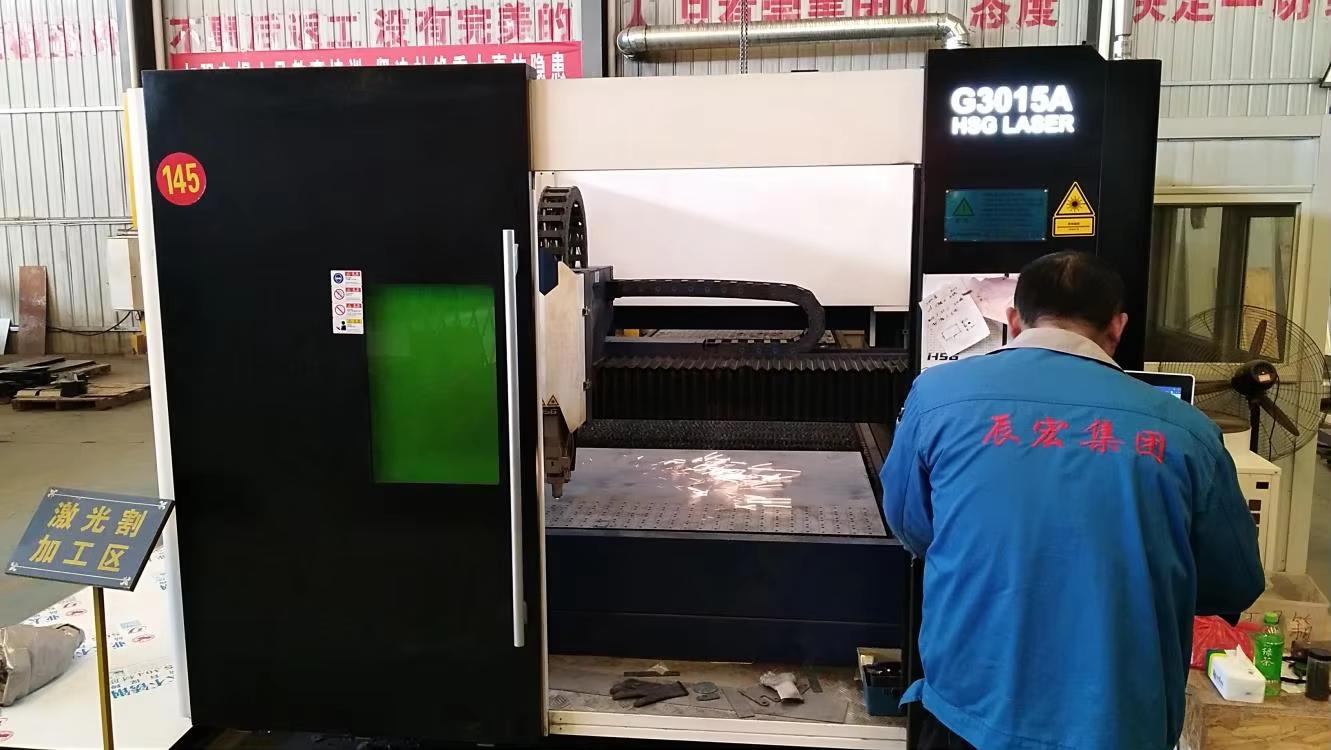
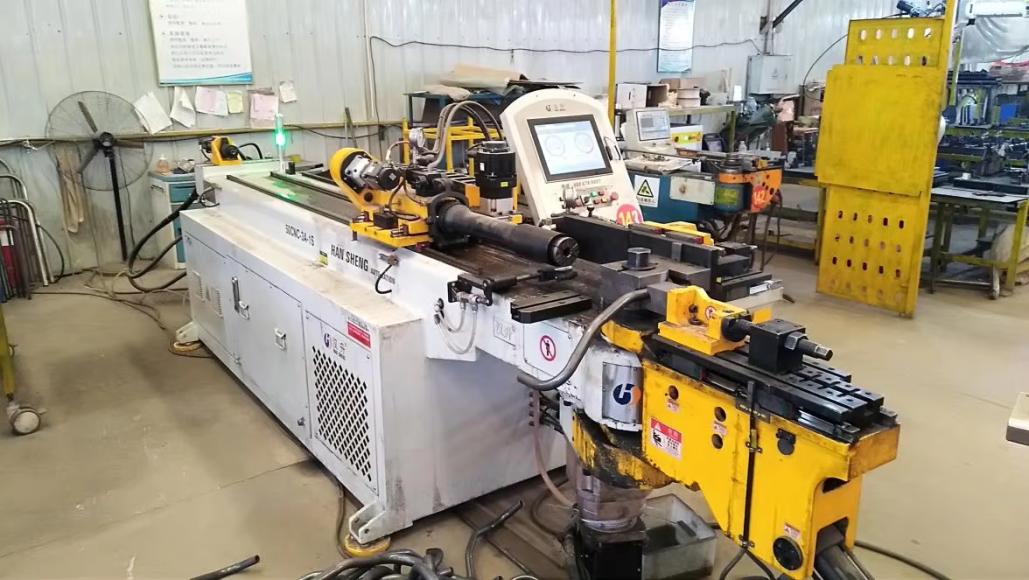
State-of-the-Art IVD Manufacturing Facility Committed to Global Quality Standards and Reliable Supply Chain Integration.
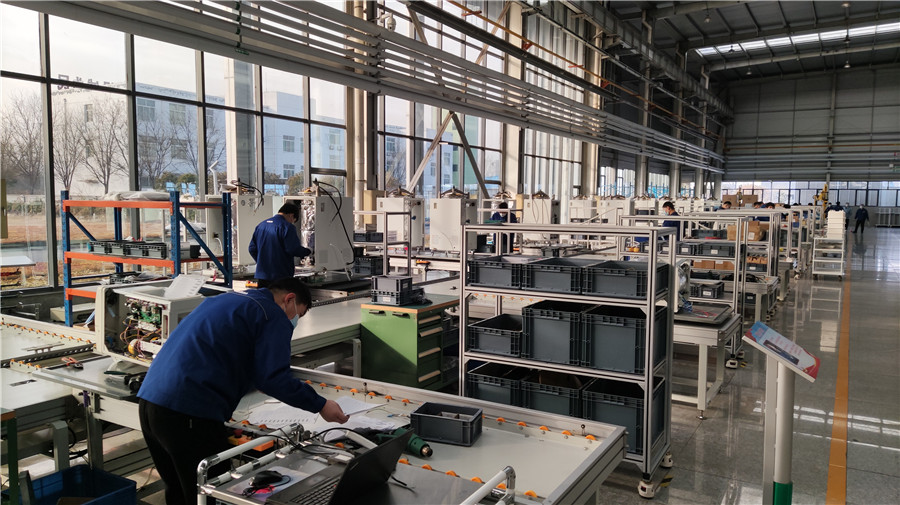
Hebei Evolve Medical Technology Co., Ltd. is a modern, rapidly expanding enterprise specializing in the research, development, high-precision automated production, and worldwide distribution of medical consumables and in-vitro diagnostic devices. The company holds Class I, II, and III medical device business licenses issued by national regulatory authorities and operates state-of-the-art facilities, including a Class 10,000 sterile laboratory and a Class 100,000 clean production workshop. These cleanrooms strictly comply with international ISO 14644 standards, preventing micro-particulate contamination during strip assembly and liquid buffer filling.
As a full-service diagnostic solution provider, Evolve Medical delivers comprehensive OEM/ODM customization solutions and turnkey procurement services for government health departments, hospital consortia, wholesale distributors, and international aid agencies serving the East African market.
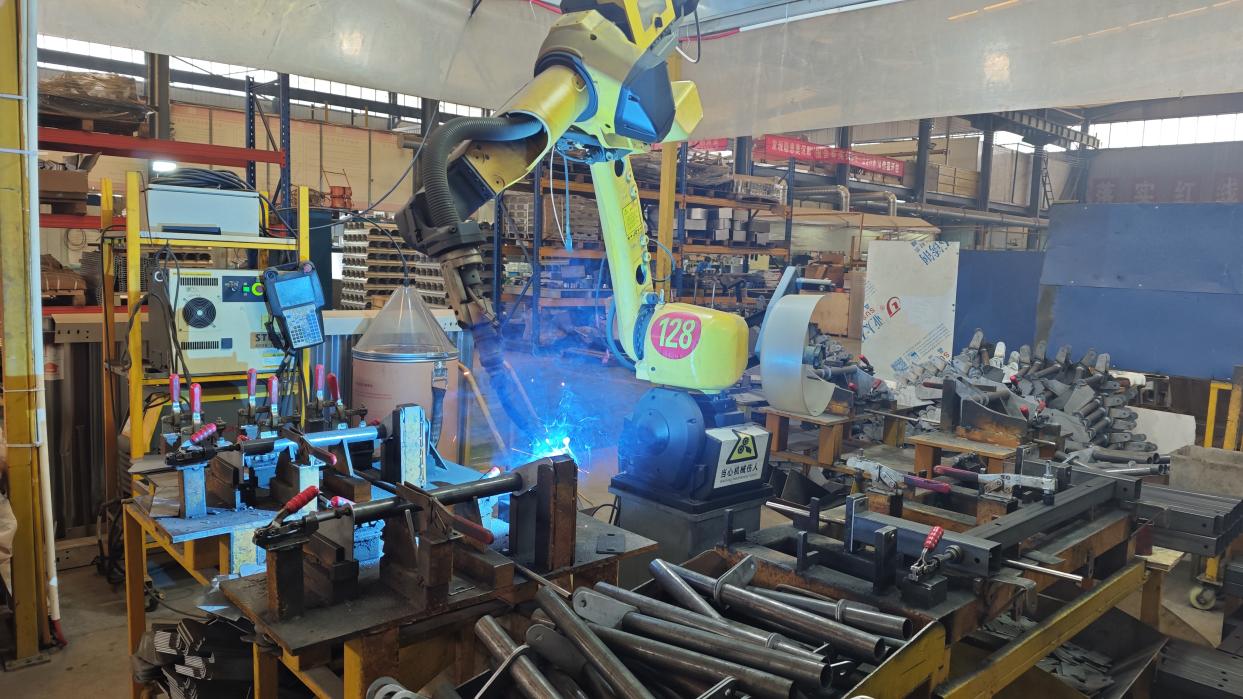
Established in 2021, Hebei Evolve Medical Technology Co., Ltd. operates multi-line automated assembly infrastructure, robotic liquid dispensing systems, and automated cassette slitting machinery.
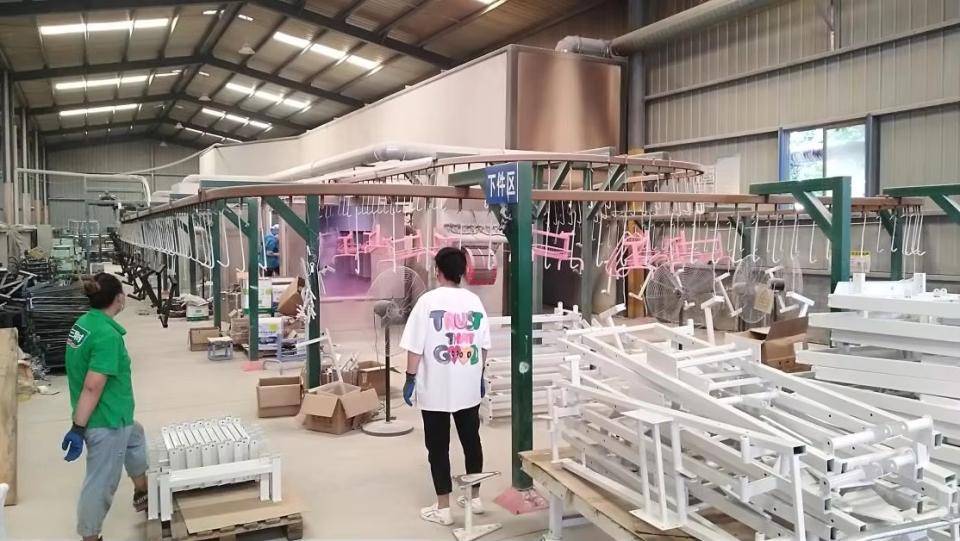
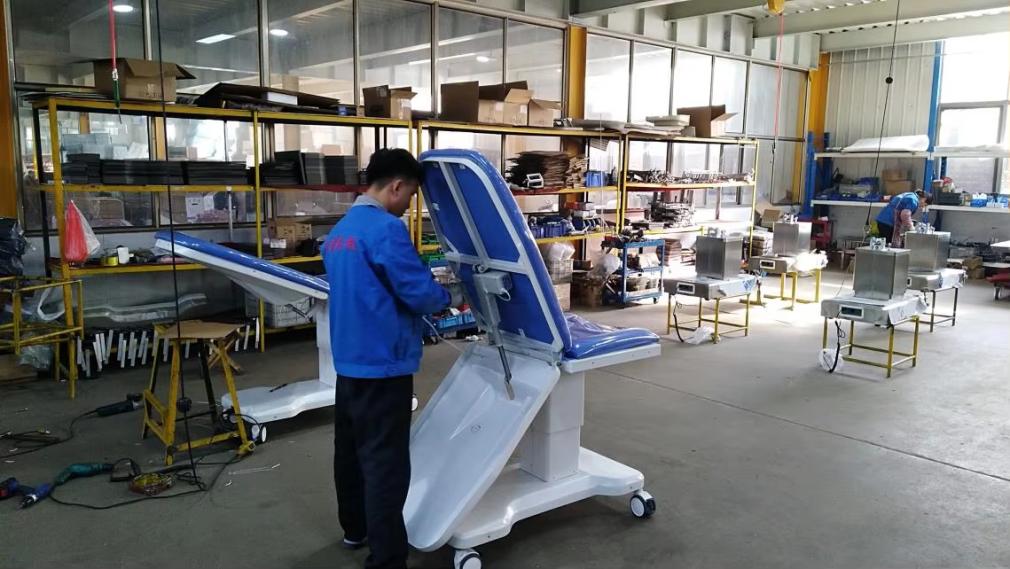
Our manufacturing processes adhere to rigid internal quality checkpoints. Guided by principles of innovation, quality control, and long-term sustainability, our engineering team monitors continuous batch consistency—from raw nitrocellulose membrane casting to final pouch sealing.
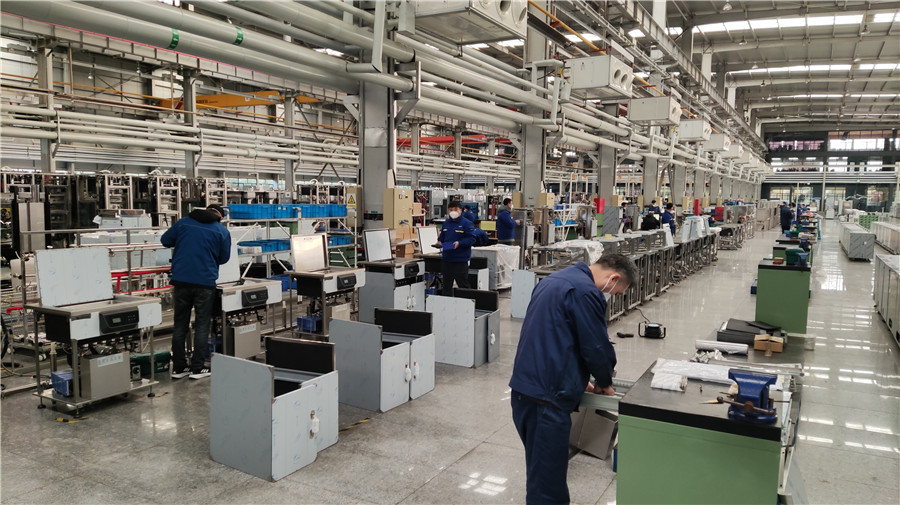
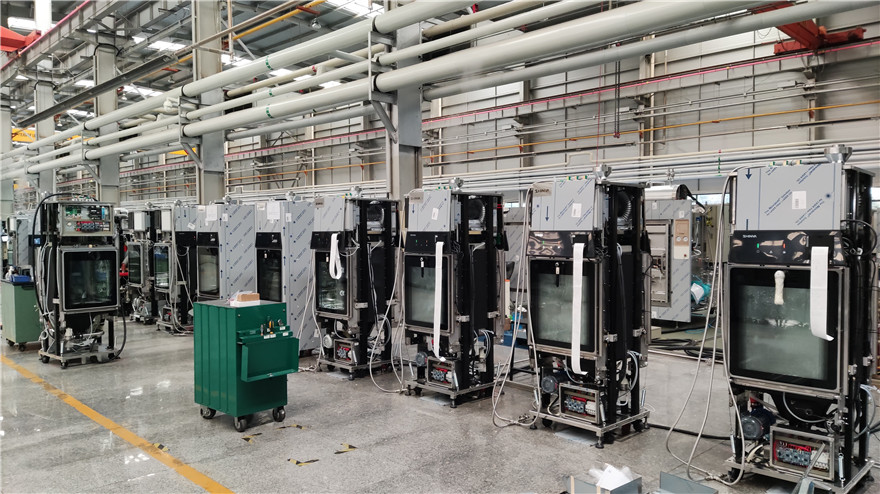
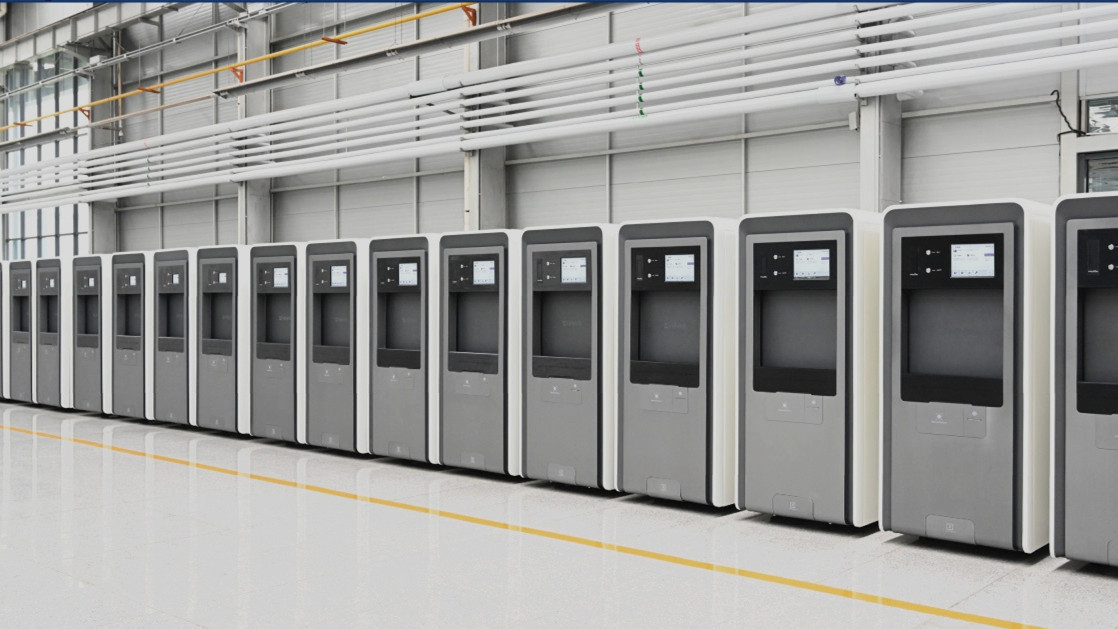
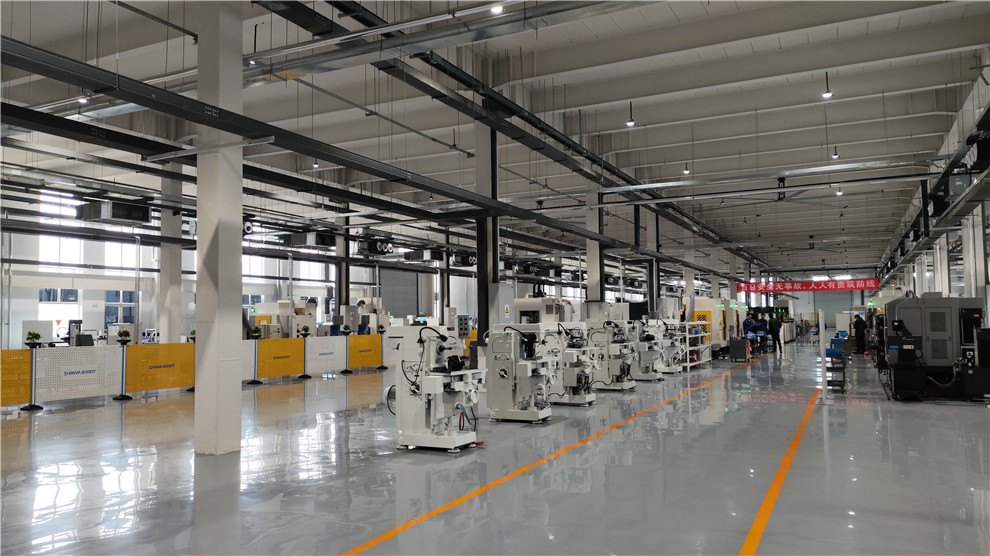
Streamlined B2B importing pathways designed for regional wholesalers, institutional tenders, and clinic networks across East Africa.
Navigating medical device import regulations in Uganda requires rigorous documentation. We provide comprehensive Dossier packages, Certificate of Free Sale (CFS), ISO 13485 audit certificates, and Batch Analysis Records (COA) to facilitate seamless clearance with the National Drug Authority (NDA) of Uganda.
Strengthen your market presence in Mbarara and Western Uganda through tailored packaging solutions. We assist regional distributors in creating custom-branded box artwork, local language inserts, specific lancet/buffer tube packaging configurations, and barcode serialization.
We manage end-to-end logistics solutions, offering flexible air freight directly to Entebbe International Airport (EBB) for express emergency stock replenishment, or sea freight to Mombasa Port with direct bonded transit trucking along the Trans-African Highway directly into Mbarara city warehouses.
Explore our full catalog of point-of-care rapid testing strips, cassettes, and extraction kits engineered for high sensitivity and rapid operational deployment.
In-depth responses for medical procurement officers, laboratory managers, and importers in Mbarara and East Africa.